CASE STUDIES / PLASTICS & PACKAGING / FINANCIAL ROI
OEE Case Study: How a Plastics Plant Recovered RM202,450 from
Hidden Downtime
An evidence-based OEE Case Study documenting how addressing hidden downtime manufacturing recovered 22% points of lost capacity and delivered an audited 3.8-month payback.
Quantified Business Payback from Real-Time Machine Telemetry
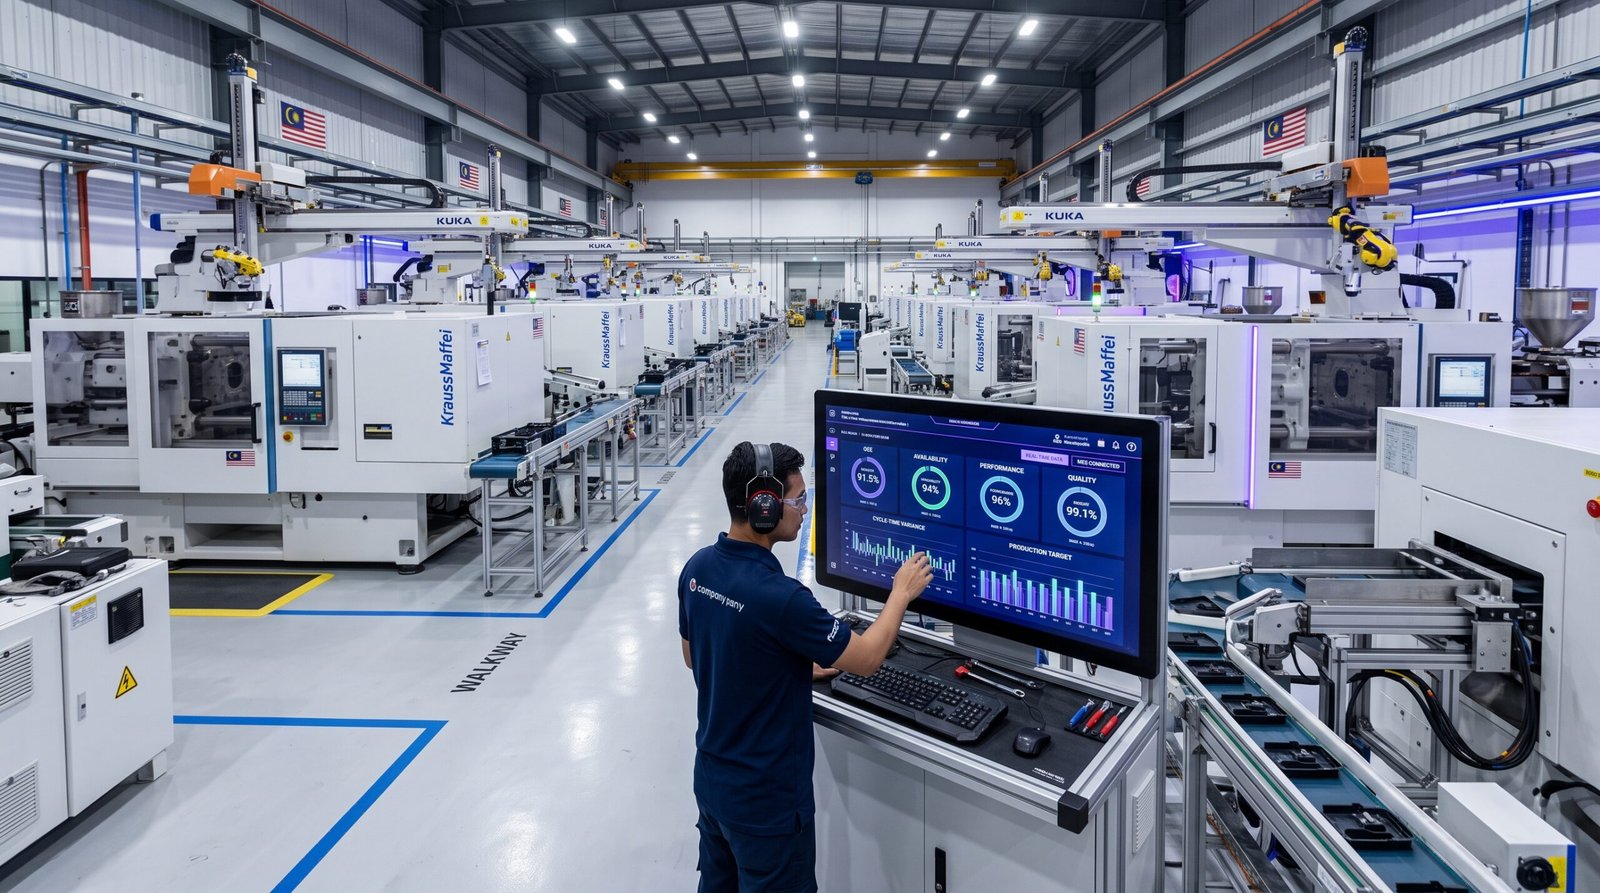
This documented Manufacturing Downtime Case Study details the elimination of unrecorded press interruptions. By transitioning from paper forms to digital telemetry in this OEE Case Study, plant leadership uncovered capacity leaks that escaped executive view.
The rigorous twelve-week audit confirmed that repetitive micro-stoppages, rather than major mechanical breakdowns, were the dominant source of margin erosion across
the Penang molding facility. Automated reason capture allowed engineering teams to correct bottlenecks within days.
RM202,450
TOTAL RECOVERED VALUE
Verified capacity recovery over 12
weeks of live tracking
22% Fewer
UNRECORDED STOPS
Short interruptions dropped from 41
daily down to 32
62% → 84%
OEE IMPROVEMENT
Gained 22 percentage points in overall
equipment efficiency
3.8 Months
MEASURED PAYBACK
Capital expenditure fully recouped from
overtime reduction
THE INVISIBLE ENEMY
How Hidden Downtime Manufacturing Erodes Plant Margins
Paper shift logs indicated the plant was operating at a respectable 85% availability. Yet
finished container shipments lagged consistently behind scheduled production quotas,
forcing frequent weekend shifts.
Shiftix hardware telemetry uncovered the root cause of hidden downtime manufacturing across the press lines. Hundreds of recurring micro-stoppages lasting between 60 and 180 seconds were quietly occurring throughout each shift.
Because each pause was brief, operators prioritized clearing part drop jams or hopper
feeds without writing them down. Small individual halts were forgotten, but collectively
they evaporated two hours of daily production capacity.
This hidden loss explains why conventional manufacturing reports fail to protect
operating margins. Shiftix automated edge sensors record every machine pulse,
ensuring no stoppage escapes accountability.
The Micro-Stoppage Compounding Cycle
Step 1: Machine Pauses (1 to 3 Minutes)
Robotic arm jam or resin feeder starvation interrupts active molding cycle.
Step 2: Unrecorded Clearing
Operator clears fault rapidly without paper logging to keep line moving.
Step 3: Data Blindspot
Event vanishes from end-of-shift whiteboard summaries and executive reviews.
Step 4: Compounded Capacity Bleed
Stoppage repeats 40+ times per day, leaking RM200k in capacity each quarter.
MEASURED DATA
Plastics Manufacturing OEE: Operational Baseline vs Optimized Output
Audited Plastics Manufacturing OEE variances recorded across 12 high-tonnage injection molding cells over 12 consecutive weeks of telemetry tracking.
Key Performance Metric
Pre-Shiftix Baseline
Post-Optimization Status
Measured Variance
Overall Equipment Effectiveness
62.0% measured baseline
84.0% verified telemetry
+22.0 percentage points
Daily Unrecorded Micro-Stops
41 average daily stops
32 stabilized daily stops
22% reduction in minor halts
Net Daily Shift Throughput
Baseline production index
+22.0% verified output volume
+22.0% net capacity recovery
Capital Payback Duration
Unmeasured paper baseline
3.8 months verified recovery
Full investment recoupment
Cumulative Value Recovered
Zero (untracked capacity loss)
RM202,450 verified recovery
Measurable shop floor ROI
Note: In strict manufacturing accounting, OEE recovery is expressed as gaining 22 percentage points (from 62% to 84%), while micro-stop frequency decreased by 22% (from 41 down to 32 daily incidents).
DIAGNOSTIC EVIDENCE
Deploying OEE Monitoring Malaysia to Diagnose Chronic Machine Stops
Digital downtime categorization eliminated speculative debates between supervisors and tooling technicians. By executing rigorous OEE Monitoring Malaysia on the press line, this specialized OEE Monitoring Malaysia deployment automatically isolated root causes with exact second-level timestamps.
40% OF ALL STOPS
Resin Hopper Feed Issues
Gravimetric loaders experienced vacuum suction
pauses and minor material bridging that starved
heating barrels for two minutes at a time.
DIAGNOSTIC FIX:
Installed level sensors and automated vacuum purge
alerts.
35% OF ALL STOPS
Robotic Take-Out Grip Jams
Slight vacuum suction cup misalignments triggered
emergency stops during container demolding, idling
the press until manual re-arming.
DIAGNOSTIC FIX:
Re-calibrated arm end-effectors and updated suction cup
materials.
25% OF ALL STOPS
Chiller Temperature Drift
Cooling mold water temperature fluctuations triggered
automated interlocks that paused cycle starts until
temperatures stabilized.
DIAGNOSTIC FIX:
Flushed secondary manifold lines and integrated chiller
loop telemetry.
STRATEGIC CAPACITY
Recovering Hidden Capacity Without Buying More Machines
“The initial operational reaction to production deficits is often requesting capital expenditure for new molding machinery or hiring temporary shifts. This OEE Case Study proved that the plant did not have a capacity shortage. It had an invisible capacity leak. The entire RM202,450 recovery was achieved using existing machines and existing personnel.”
By unlocking 22 percentage points of lost OEE, the factory absorbed two new packaging container product lines without adding a single machine to the floor plan.
Avoiding unnecessary equipment purchases saved an estimated RM1.4 million in deferred capital machinery investments, floor space reconfiguration, and power substation
upgrades.
AUDITED FORMULA
How the RM202,450 Financial Recovery Was Calculated
Engineering credibility requires complete calculation transparency. Within this OEE Case Study, the OEE Monitoring Malaysia calculated based on recovered productive machine hours multiplied by the plant standard hourly manufacturing rate.
Recovered Operating Machine Hours × Standard Manufacturing Value Per Hour = RM202,450 Recovered Production Value.
Eliminated Weekend Overtime
Prevented 168 hours of premium wage overtime shifts across
three manufacturing cells.
Scrap & Purge Material Savings
Avoided resin thermal degradation in heated barrels during
unrecorded idle periods.
Absorbed Customer Backlog
Delivered committed container volumes on time, avoiding
contractual air-freight penalties.
EXECUTIVE TAKEAWAYS
Key Takeaways from This OEE Case Study
Lesson 01:
Paper records create an artificial sense of operational security by omitting micro-stops under three minutes.
Lesson 02:
Automated telemetry captures objective timestamps that eliminate subjective fault debates between shifts.
Lesson 03:
Digital downtime categorization enables maintenance teams to solve recurring mechanical feeder root causes.
Lesson 04:
Production capacity should always be recovered from existing assets before evaluating new capital equipment purchases.
Lesson 05:
Deploying dedicated OEE Monitoring Malaysia delivers verifiable return on investment within four months of stabilization, as confirmed by this manufacturing downtime case study.
Clear operational answers on micro-stop tracking, plastics line OEE calculation, and real-world capital payback.
Why is this OEE Case Study focused specifically on short micro-stoppages?
Most plants only record breakdowns exceeding 15 minutes on whiteboards. As shown in this OEE Case Study, unrecorded stops lasting 1 to 3 minutes happen dozens of times per shift, quietly draining hours of press capacity without management ever noticing.
How does Shiftix eliminate hidden downtime manufacturing in plastics plants?
To eliminate hidden downtime manufacturing, Shiftix connects non-invasive optical and CT sensors directly to injection presses. This elevates baseline Plastics Manufacturing OEE by capturing sub-minute robotic take-out halts and hopper feed starvations automatically.
How was the RM202,450 financial recovery calculated in this study?
This manufacturing downtime case study calculates payback by multiplying recovered machine hours by the plant standard operating value. Unlocking 22 percentage points in OEE allowed the factory to fulfill extra orders without adding new machines or hiring more operators.
Can Malaysian plastics processors claim MIDA grants for this deployment?
Yes. Implementing OEE Monitoring Malaysia qualifies for up to 70% matching grant funding under MIDA Industry4WRD digitalization schemes, covering both hardware telemetry gateways and software licensing.
Find Your Factory's Hidden 3-Minute Leaks
You don’t need to purchase more machines to increase output. Let our OEE Monitoring Malaysia system to audit your shop floor telemetry and uncover the hidden downtime draining your plant capacity.