CASE STUDIES / PRECISION MANUFACTURING / OEE OPTIMIZATION
A leading Malaysian tier-1 automotive and precision component manufacturer deployed Shiftix OEE Monitoring Malaysia to uncover hidden micro-stoppages, optimize tool changeovers, and recover 18% lost line capacity in 90 days.
INDUSTRY
Precision Metal & Stamping
LOCATION
Shah Alam, Selangor, Malaysia
DEPLOYMENT SCOPE
16 CNC & Stamping Press Lines
TIMELINE
8 Weeks from Audit to Go-Live
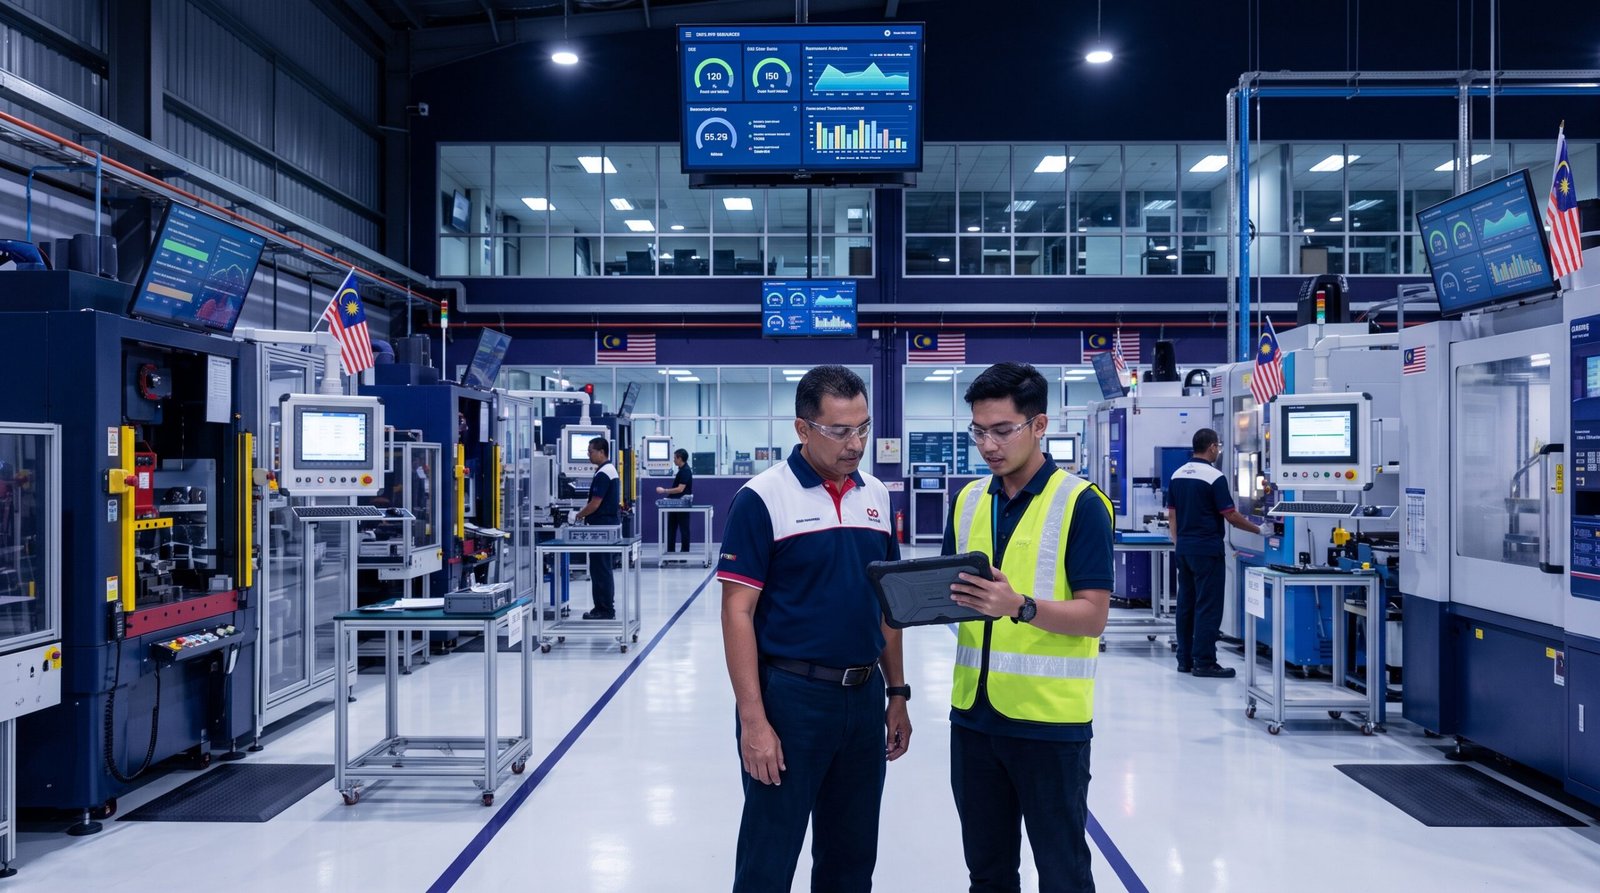
Figure 1.0: Real-Time Machine Telemetry & OEE Dashboard Deployment on Malaysian Press Lines
VERIFIED SHOP FLOOR DATA
AT A GLANCE
Prior to digitalization, the plant operated under the assumption that overall equipment effectiveness hovered around 72%. Shiftix machine telemetry revealed actual baseline OEE was 54% due to unrecorded micro-stops and uncoordinated die changes. Within three months of automated tracking, deploying OEE Monitoring Malaysia eliminated RM200,000 in scrap and unplanned overtime.
NET ANNUAL COST AVOIDANCE
TOTAL OEE RECOVERY
SMED CHANGEOVER DURATION
AUTOMATED REASON LOGGING
THE CHALLENGE
Before adopting dedicated OEE Monitoring Malaysia architecture, the manufacturing facility produced high-volume precision stamped brackets, the manufacturing facility produced high-volume precision stamped brackets and motor housings across two operating shifts. While production quotas appeared on track, plant leadership faced escalating overtime wage bills and frequent weekend shifts to meet customer delivery commitments.
Machine operators recorded operational downtime manually on paper shift forms. Stoppages under five minutes such as feeder strip jams, sensor misalignment, and air pressure dips were routinely omitted because operators prioritized clearing the fault over clerical logging.
Unrecorded Micro-Stops
Loss: High
Prolonged Tooling Changeovers
Variance: 75%
Delayed Maintenance Response
Latency: 45 min
THE SOLUTION
Deploying OEE Monitoring Malaysia requires moving beyond disconnected paper logs to automated Manufacturing Downtime Tracking. Our dedicated Machine Telemetry MES captures run, idle, and micro-stop intervals in real time, unlocking full shop floor transparency.
HARDWARE LAYER
Non-Invasive PLC & Sensor Interfacing
SHOP FLOOR LAYER
Operator Digital Tablet Terminals
MANAGEMENT LAYER
Live OEE Dashboards & Andon Alerts
IMPLEMENTATION METHODOLOGY
Rapid deployment was essential to prevent disruption to automotive OEM delivery schedules. Shiftix engineered a non-invasive staging methodology that allowed each stamping cell to be instrumented and verified during routine weekend maintenance windows.
PHASE 01
WEEKS 1-2
Audit & Signal Mapping
Mapped electrical schematics across all 16 presses and defined standardized factory downtime taxonomy codes. Engineers validated auxiliary sensor mount points without cutting factory power lines.
✓ Schematics Verified
PHASE 02
WEEKS 3-4
Pilot Line Deployment
✓ 0% Stroke Discrepancy
PHASE 03
WEEKS 5-6
Floor Training & Calibration
✓ 35 Operators Certified
PHASE 04
WEEKS 7-8
Full Rollout & ERP Sync
Connected all 16 machines to Shiftix centralized cloud telemetry for continuous OEE Monitoring Malaysia and synchronized verified production counts with top-floor ERP. Daily automated OEE summaries were routed directly to executive manufacturing leadership.
✓ Complete Factory Go-Live
BUSINESS VALUE
Detailed audited savings accumulated over the initial 12-month operational period following system stabilization.
The verified financial returns in this Plant OEE Improvement Case Study prove that robust OEE Monitoring Malaysia delivers clear Shop Floor Digitalization ROI. Real-time data replaces subjective guesswork, enabling continuous throughput gains.
| Operational Cost Factor | Pre-Implementation Baseline | Post-Shiftix Optimization | Annual Financial Impact |
|---|---|---|---|
| Unplanned Overtime Wages | 38 monthly overtime hours per operator | Reduced to under 8 monthly hours | RM84,000 saved in overtime payroll |
| Die & Tooling Scrap Rates | 3.8% raw coil scrap from misfeeds | Stabilized below 1.2% total scrap | RM68,000 in raw material recovery |
| SMED Changeover Downtime | 55 minutes average die swap | 32 minutes pre-staged changeovers | RM32,000 in recovered machine hours |
| Preventative Tool Breakage | 7 catastrophic die failures per year | Zero major tool crashes recorded | RM16,000 avoided die repair costs |
| Total Annual Cost Savings | Verified Baseline Losses | Continuous OEE Optimization | RM200,000 Net Annual Savings |
Long-Term Cultural Transformation on the Stamping Floor
With 18% recovered line capacity driven by OEE Monitoring Malaysia, the plant successfully onboarded two new automotive component programs without purchasing additional machinery or expanding floor space. The entire capital investment in Shiftix was fully recouped within five months of operational go-live.
Implementing systematic OEE Monitoring Malaysia has established a culture of data-driven collaboration across the Shah Alam stamping plant. Supported by scalable Machine Telemetry MES, the facility continues to hit peak output targets with predictable line availability.
Industrial Telemetry Audit Completed
Verified by Shiftix Manufacturing Solutions Division, Shah Alam Hub
Case ID: SX-OEE-MY-200K
FREQUENTLY ASKED QUESTIONS
Practical operational insights on downtime tracking, non-invasive machine telemetry, and capital payback.
Most precision metal and stamping facilities recover their initial investment within three to six months. By identifying chronic micro-stoppages and reducing changeover delays, plants capture substantial line capacity without purchasing additional machinery.
Our Machine Telemetry MES architecture integrates seamlessly with both modern PLCs and legacy equipment. We deploy non-invasive IoT sensors and current transducers to capture run, idle, and fault states on machines operating for over twenty years without altering electrical schematics.
Automated tracking replaces subjective shift logs with verifiable timestamps. Machine operators categorize stoppage causes via single-touch workstation tablets, enabling engineering teams to resolve chronic mechanical bottlenecks rather than debating fault allocation.
Yes. Hardware gateways, digital operator touchscreens, and software subscription costs for smart factory digitalization qualify for up to 70% matching grant incentives under Malaysian government Industry4WRD programs.
Unrecorded micro-stops and uncoordinated tooling changeovers quietly drain thousands of ringgit every month. Speak with our manufacturing engineers to benchmark your current OEE baseline and identify verifiable cost savings across your production lines.